Incoming materials
Critical films, adhesives, inks, circuits and components are identified from the BOM.
Evidence matched to the approved product
Quality planning begins with measurable drawing requirements and a defined inspection method. Visual, dimensional, electrical and functional checks are selected for the approved component; certificates and reports remain linked to the actual holder and tested item.
Engineering variables
Critical films, adhesives, inks, circuits and components are identified from the BOM.
Printing, registration, lamination, die cutting and assembly checkpoints are defined.
Appearance, dimensions, circuit continuity and project-specific functions are checked.
Drawing revision, lot information and retained evidence are matched to the agreed scope.
Decision matrix
A useful quality plan names the approved product revision, characteristic, specimen, method, equipment, sampling or coverage, acceptance limit and record owner before inspection begins. Results apply only to the identified item and conditions; component evidence does not establish finished-equipment certification or system validation.
| Decision factor | Quality-plan definition | Evidence returned |
|---|---|---|
| Product and revision identity | Identify the approved drawing, artwork, BOM or controlled construction, part and revision, project stage, lot or sample identity, and every accepted deviation before inspection begins. | Tie the inspection record to the exact source item, revision, lot and specimen. An unapproved substitution, superseded file or unidentified sample cannot support acceptance of the released product. |
| Critical characteristics and limits | Name visual zones, dimensions and tolerances, print registration, key feel or functional states, circuit and connector checks, plus every customer-designated critical item. Give each characteristic a measurable limit or an agreed judgement method. | Return a check plan that separates measured values from visual and functional judgements, then records pass, fail or conditional status with unresolved items visible rather than converted into a general quality claim. |
| Sampling and coverage | Define the lot, inspection unit, characteristic risk, destructive or non-destructive method, sample selection, size and acceptance or rejection rule, or identify the characteristic that requires 100% coverage. | State the inspected population, selected sample or coverage and resulting lot disposition. There is no universal AQL, sample size or switching rule that truthfully fits every product, characteristic and customer risk. |
| Measurement and equipment | Define the method, fixture, equipment range and resolution, calibration or verification status, environment and operator information needed for the characteristic and tolerance. | Record the method, equipment identity and status, date and any relevant uncertainty or limitation. Out-of-range, expired, unsuitable or unidentified measurement evidence cannot prove acceptance. |
| Electrical, functional and assembly checks | Provide the circuit map or pinout, applied electrical conditions and sequence, connector mating definition, enclosure and mounting condition, lighting or indicator logic, and the expected control behaviour. | Tie continuity, functional and installed-assembly results to the named specimen and test conditions. These component results do not prove system electrical safety, EMC, enclosure performance or complete-equipment compliance. |
| Special validation, traceability and release | Name any customer or industry test method, conditioning, sequence, duration, specimen count, acceptance criterion, report format, traceability, change-notification rule and approval owner. | Issue a report that identifies the sample revision, method, actual results, deviations, disposition and decision owner. Do not generalize the result beyond the tested method, assembly, revision and stated conditions. |
The ISO references below provide sampling, measurement-management and laboratory-competence context only. They do not prove that HYR, the parent company, a test provider or a proposed product is certified or accredited, or that a component result establishes finished-equipment compliance.
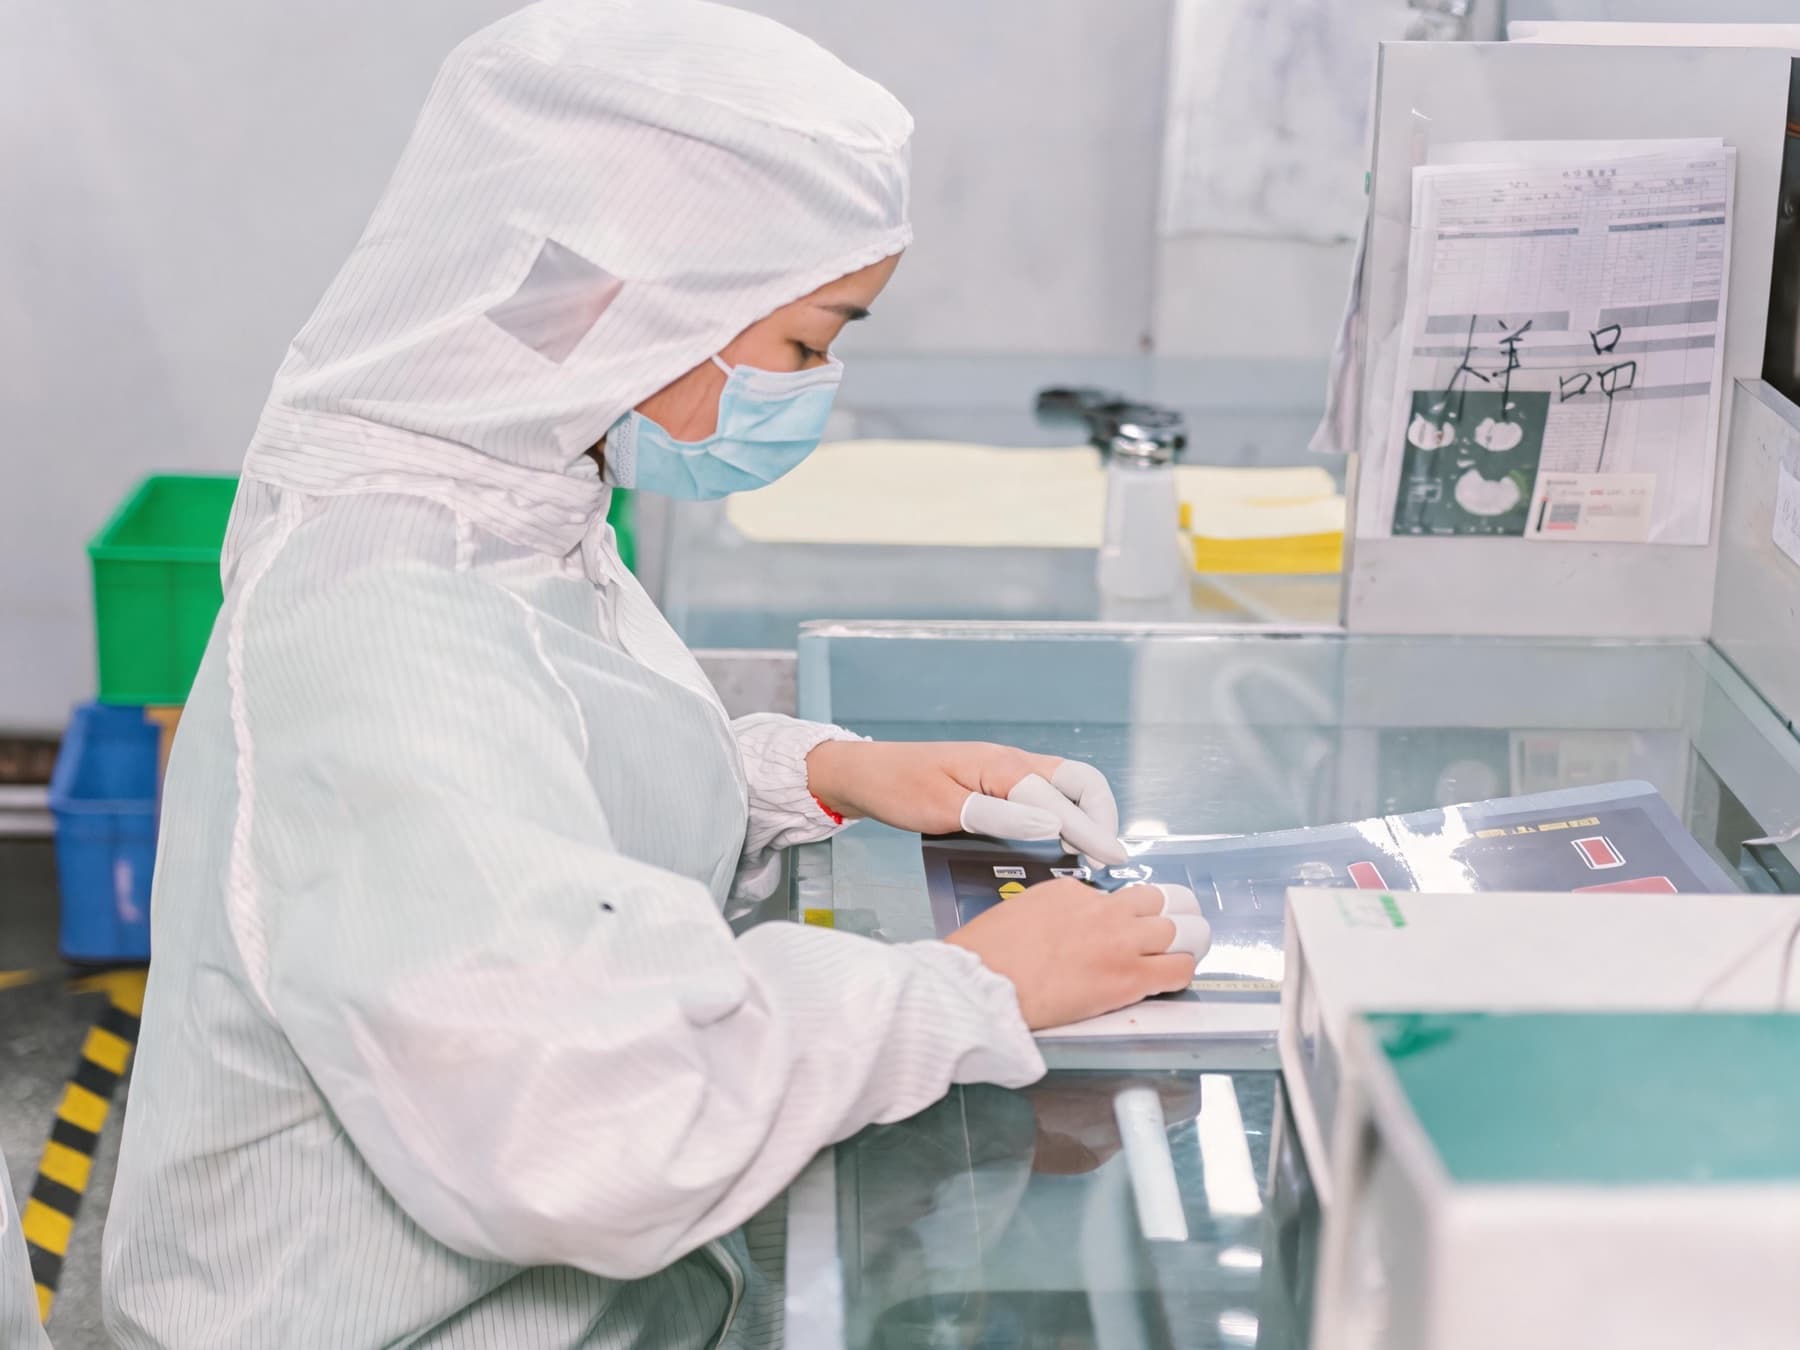
Real product evidence
Real quality resource provided by Shenzhen Baoshengda Technology Co., Ltd., the parent company of HYR FLEX.
Representative product resource · project construction is confirmed from the approved drawing.Documents you can verify
Certificate holder: Shenzhen Baoshengda Technology Co., Ltd.. These certificates belong to the parent company, not to HYR FLEX or Shenzhen Huayangrun Technology Co., Ltd.
CEPREI Certification Body
The stated scope is manufacturing; this is not product certification.
CEPREI Certification Body
Exclusions: Product Design. IATF USI: 3M6E49.
Covered manufacturing site: North plant, 2/F, Building A2, Yijing Industrial Park, No. 3055 Songbai Road, Tianliao Community, Gongming Street, Guangming New District, Shenzhen, Guangdong, China.
Continuing validity depends on satisfactory surveillance audits. Recheck the issuer record for supplier approval. Management-system certification does not establish product performance, an IP rating, medical-device approval or conformity of an OEM's finished equipment. The CNAS mark on the ISO certificate concerns the certification body's accreditation, not a claim that HYR operates a CNAS-accredited laboratory.
Request a project-specific supplier evidence pack ↗Before the RFQ
Start with the evidence you have now. Open items stay visible for engineering follow-up instead of becoming silent quotation assumptions.
No. The sampling basis must match the defined lot, characteristic, inspection method, consequence of nonconformity and customer agreement. Some characteristics can use an agreed acceptance-sampling plan; others may require 100% inspection, a destructive sample or a separate validation activity.
No. A certificate or report supports only its named holder, material, lot, method, result, validity and scope. The assembled membrane switch still needs evidence tied to its controlled construction and the characteristics the customer intends to accept.
No. Membrane-switch evidence can support the identified component and installed checks, but system electrical safety, EMC, enclosure performance, software behaviour, regulatory approval and finished-equipment validation remain with the OEM unless responsibilities and evidence are separately defined.
A useful fit when
Limits to resolve
Prepare the RFQ
You can submit what is available now. Unknown items remain visible for human follow-up rather than being guessed.
Critical-to-quality characteristics
Required inspection method or report
Sampling or traceability expectation
Customer acceptance criteria
Evidence boundary
Only verified, in-scope records are used. Parent-company certificates are shown as parent-company evidence and never relabelled as HYR certificates.
Technical reference basis
These publisher resources support the decision framework. They do not prove that HYR uses a named grade, holds a listed certification or has approved a project construction.
Official context for AQL-indexed lot-by-lot acceptance-sampling schemes; not evidence that one plan applies to every HYR project or that any proposed lot has been accepted.
Official context for confidence in measurement processes and results; not evidence that HYR operates a certified measurement management system or that project measurements are valid without their own records.
Official laboratory-competence and accreditation context; not evidence that HYR, its parent company or a proposed test provider is accredited, or that a named report is within an accredited scope.